Best China Industrial Roller Conveyor Product, Manufacturer
At Hangzhou Aotuo, we understand that every industry has unique challenges, which is why our solutions are customizable to fit your specific requirements. Our Industrial Chain Conveyor systems are a perfect example of this adaptability, engineered to efficiently transport materials in a variety of settings. Whether you are looking to streamline your assembly line or enhance your material handling processes, our expert team is dedicated to delivering the right solutions to meet your needs. By partnering with us, you gain access to high-quality products, competitive pricing, and unwavering support, making Hangzhou Aotuo your ideal partner in achieving industrial excellence

Why Trust Industrial Roller Conveyor Outperforms the Competition Stands Out
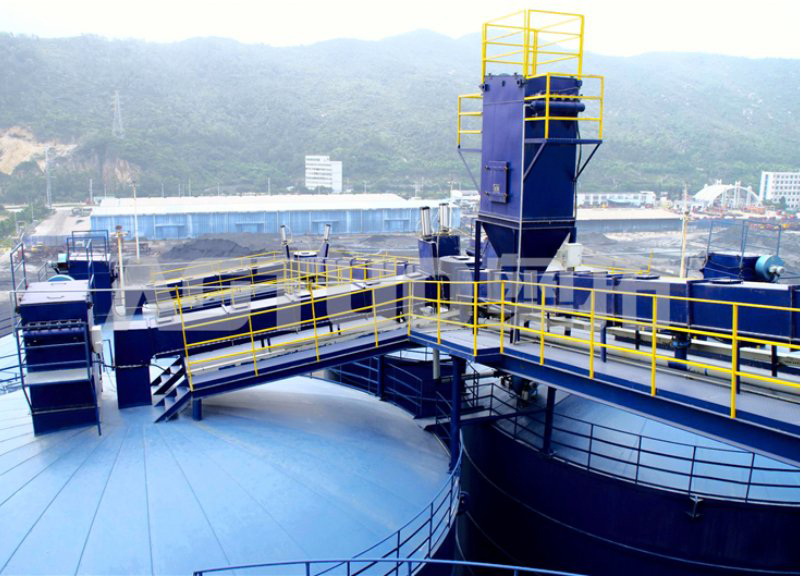
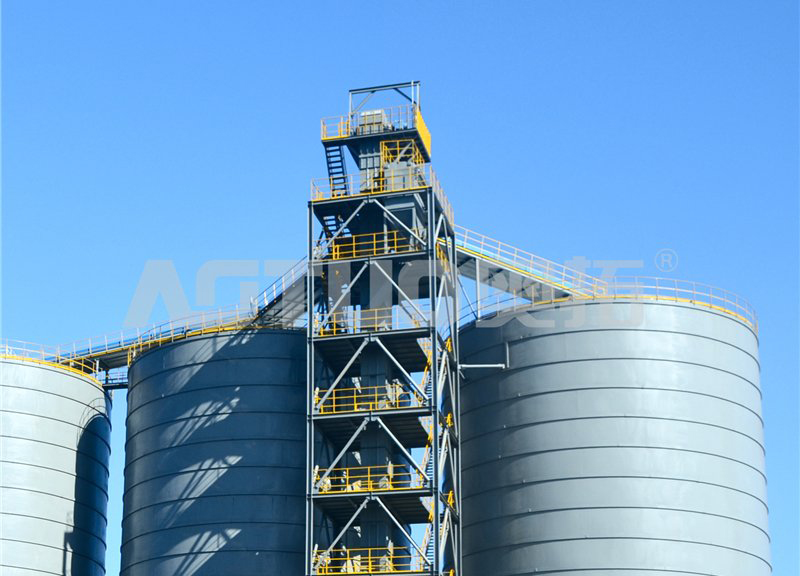
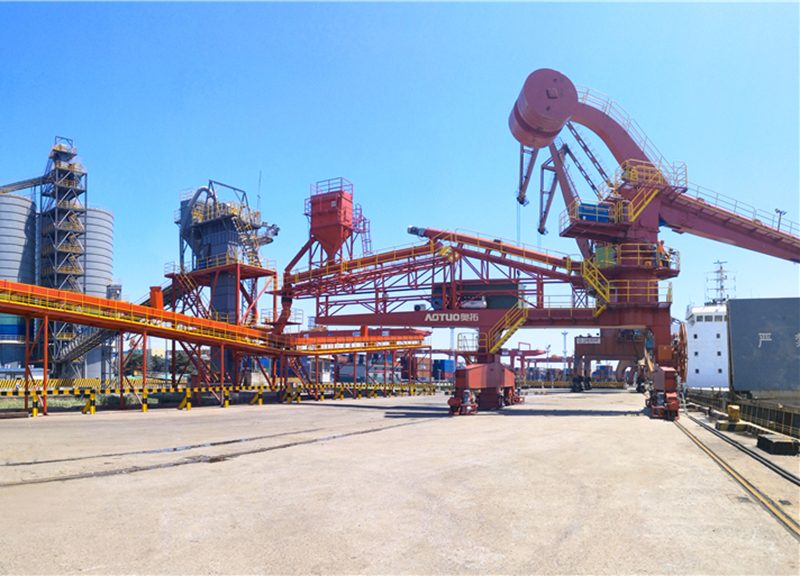
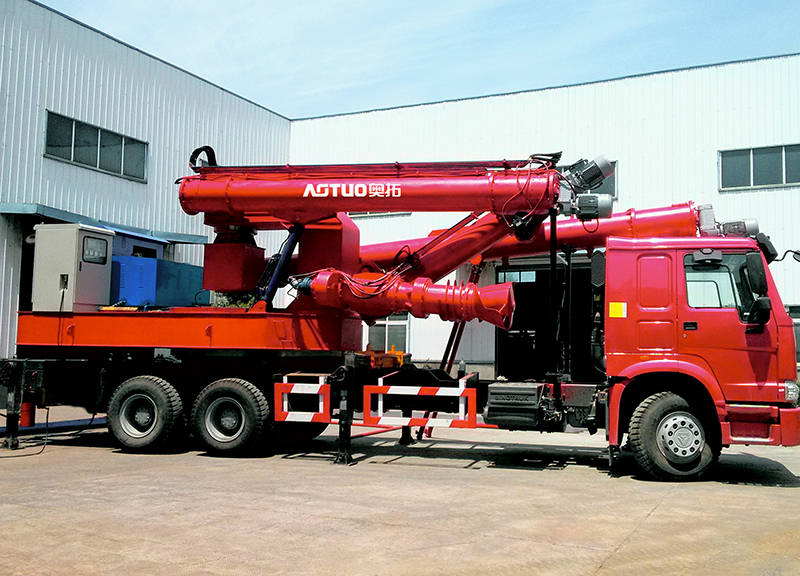
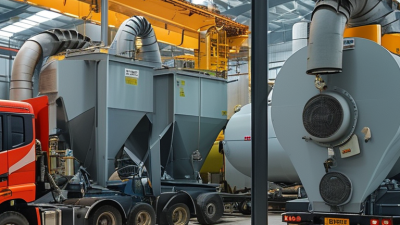
In today's competitive market, it’s crucial for industries to adopt advanced solutions that streamline operations and enhance productivity. Industrial Roller Conveyor systems have emerged as a superior choice, particularly in the handling of bulk materials like sawdust and ash. Among the various options available, screw conveyors are particularly effective for transporting dry bulk materials, thanks to their efficient design and versatility. Whether dealing with screw elevator conveyors or ash conveyor systems, businesses can expect increased efficiency and reliability in material handling processes.
Moreover, the integration of advanced technology in conveyor systems has led to improved dust collection solutions. High-performance dust extraction systems, including dust collector fans and dry dust collectors, play a pivotal role in maintaining a clean workspace. The presence of a dust collection unit, combined with innovative designs like the dust deputy bucket and specialized dust collector bags, ensures that industries can meet health and safety standards while keeping operations smooth. For specialized tasks, such as wood processing or metal handling, customized solutions like the sawdust vacuum system and lathe dust collection setups provide additional effectiveness in dust management.
Ultimately, choosing reliable conveyor systems and effective dust collection technologies is essential for any global purchaser aiming to optimize their industrial processes. Investing in robust equipment, such as the flexible belt conveyor or gravity feed conveyor, can lead to significant long-term savings and operational success. This ensures a streamlined workflow, not only in transporting materials efficiently but also in managing the byproducts that arise during industrial processes. As industries move forward, leveraging cutting-edge conveyor solutions and dust extraction systems will undoubtedly set companies apart from the competition.
Why Trust Industrial Roller Conveyor Outperforms the Competition Stands Out
| Dimension | 2023 Market Trend | 2024 Market Forecast | Growth Rate (%) |
|---|---|---|---|
| Global Conveyor System Market Size | $7.53 Billion | $8.60 Billion | 14.2% |
| E-commerce Influence | High Demand for Automation | Continued Growth & Investment | Increase of 20% |
| Manufacturing Sector Growth | 7% Growth Annually | Projected 8% Growth | Increased Demand for Efficiency |
| Emerging Technologies | Integration of IoT | Higher Adoption Rates | Projected Growth of 25% |
Why Opt For Industrial Roller Conveyor Market Leader Dominates
J
James Peters
This product is top-notch! The craftsmanship is exquisite, and the staff’s professionalism made the transaction smooth and enjoyable.
25
May
2026
W
William Thomas
Very happy with my purchase! The product quality is high, and the customer service team displayed great professionalism and knowledge.
26
May
2026
G
Grace Allen
This product stands out for its quality. I also appreciated the attentive customer service, making me feel valued as a client.
27
May
2026
N
Noah Phillips
This product exceeded my expectations! The professionalism of the after-sales staff was a huge plus in my buying experience.
13
May
2026
L
Lucas Martinez
Impressive quality across the board. The support after my purchase was exceptional and very professional.
17
April
2026
M
Mark James
Impressive quality and functionality! The team was knowledgeable and ensured I was well taken care of after my purchase.
27
May
2026