Best High-Quality Conveying Systems Construction Factory, Product
Hangzhou Aotuo Mechanical and Electrical Co., Ltd. proudly stands as a leading manufacturer of high-quality conveying systems, dedicated to providing innovative solutions for various industries worldwide. With years of expertise in the realm of mechanical and electrical engineering, our factory specializes in the design and construction of advanced systems, including top-of-the-line Construction Conveyor systems and effective Dust Collector Construction. We understand the critical role that efficient material handling and dust management play in enhancing productivity and maintaining safety in construction settings. By combining cutting-edge technology with sustainable practices, we ensure that our products meet the highest industry standards while delivering optimal performance

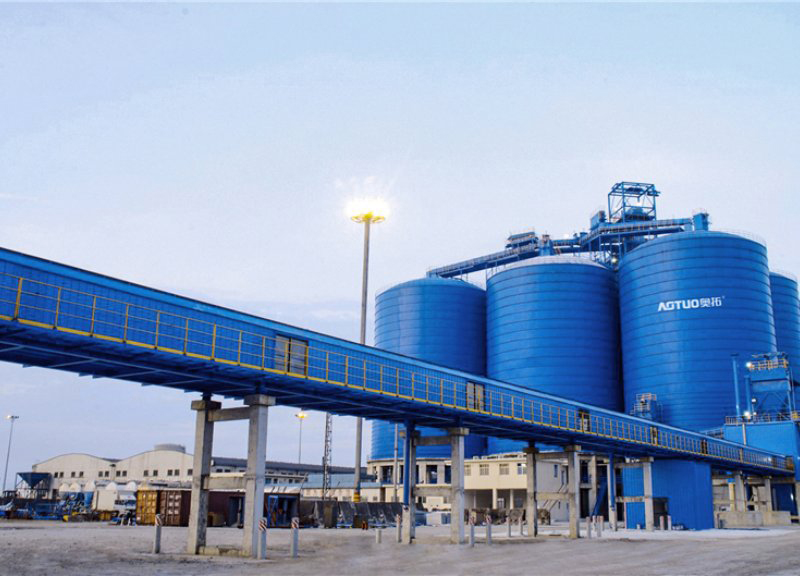
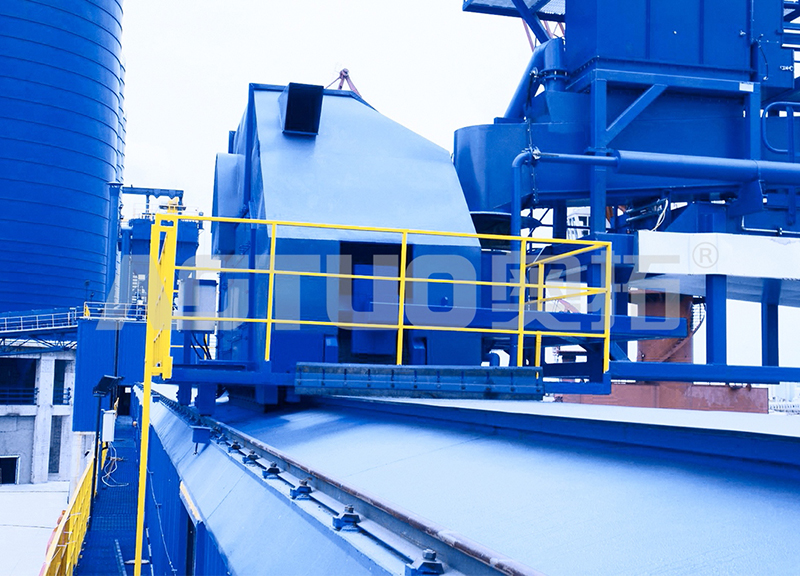
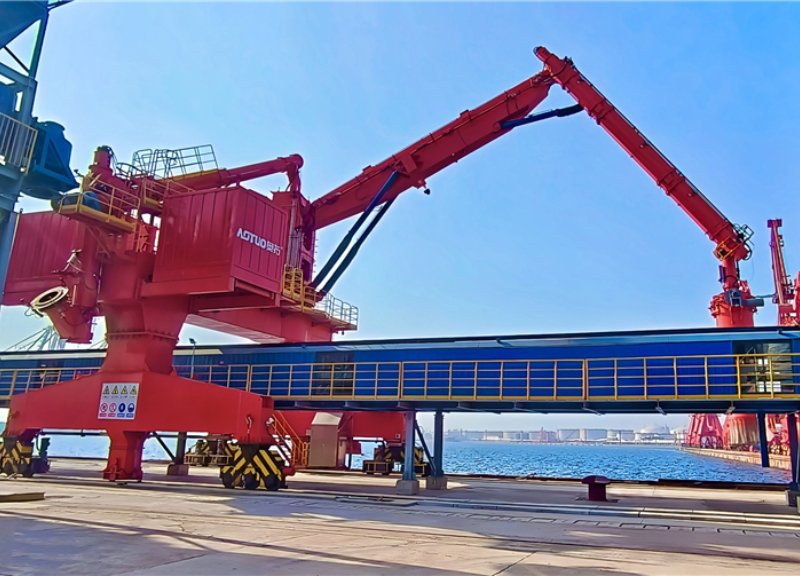
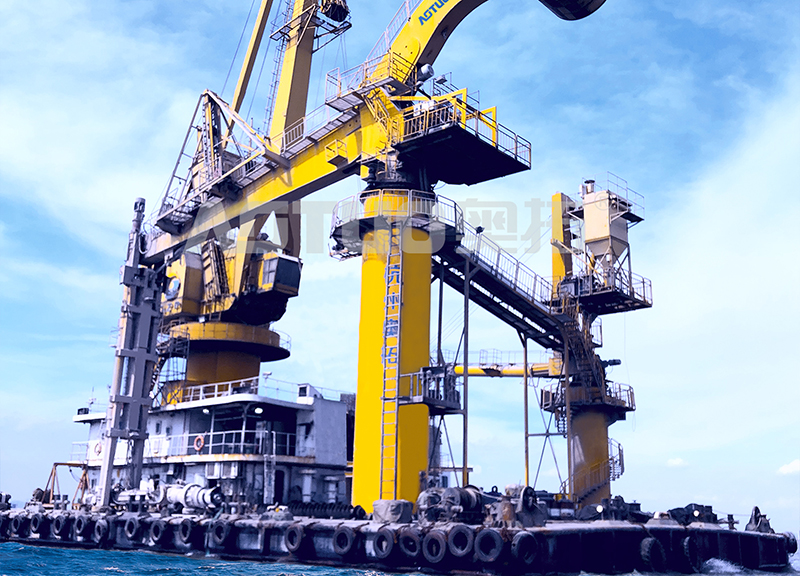
How To Select Conveying Systems Construction Exceeds Industry Benchmarks Factory-Direct Excellence
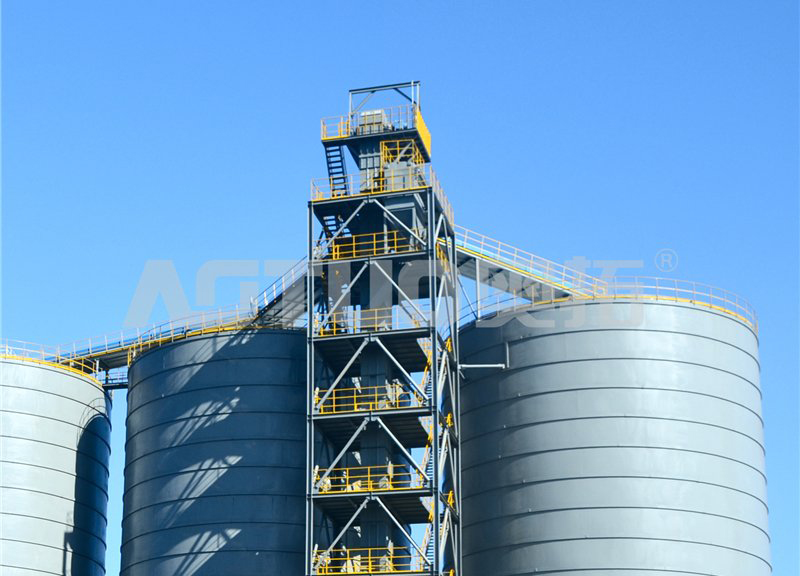
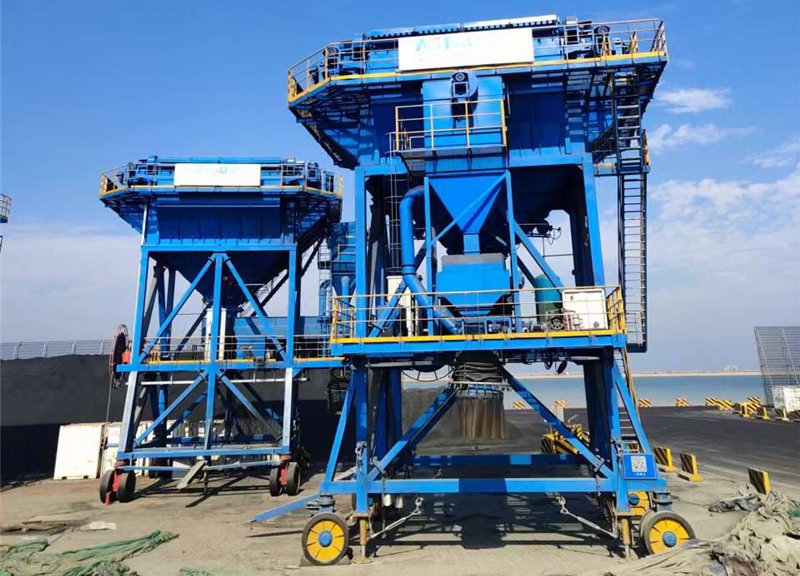
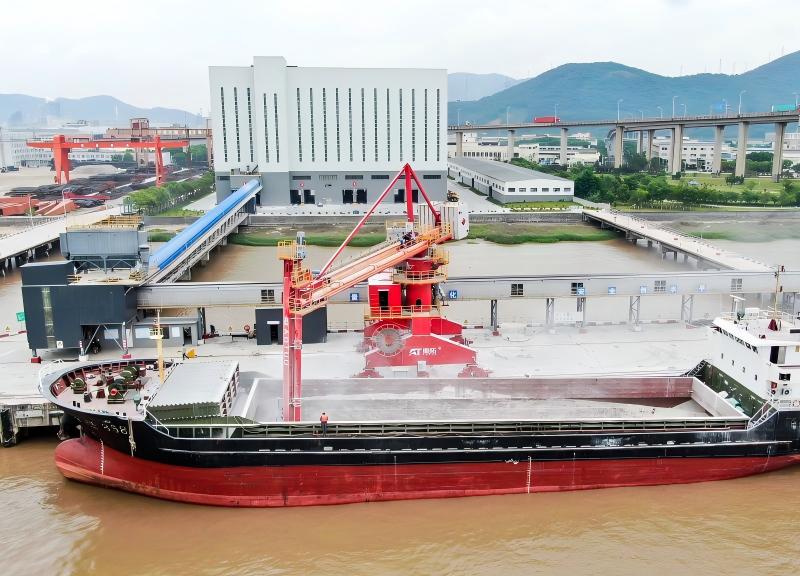
When selecting conveying systems for your operations, it's crucial to understand the various types available and the specific requirements your facility may have. Systems such as the Screw Elevator Conveyor and Ash Conveyor Systems demonstrate versatility and efficiency in handling diverse materials. The right selection not only improves operational efficiency but also meets or exceeds industry benchmarks, ensuring that you are equipped with factory-direct excellence that is cost-effective and reliable.
Integrating Conveyor Systems into your factory setup can streamline your material handling processes. From Lift Conveyor Systems designed to elevate materials safely to Air Conveyor Systems that facilitate high-speed movement of lightweight products, understanding the functionalities is key. It’s also important to consider supporting equipment, like Dust Collector Bag systems that maintain clean working environments while optimizing collection efficiency with rates specified by Dust Collector Cfm metrics. By investing in advanced conveying technology, including Flexible Belt Conveyor options, businesses ensure operational effectiveness and environmental compliance.
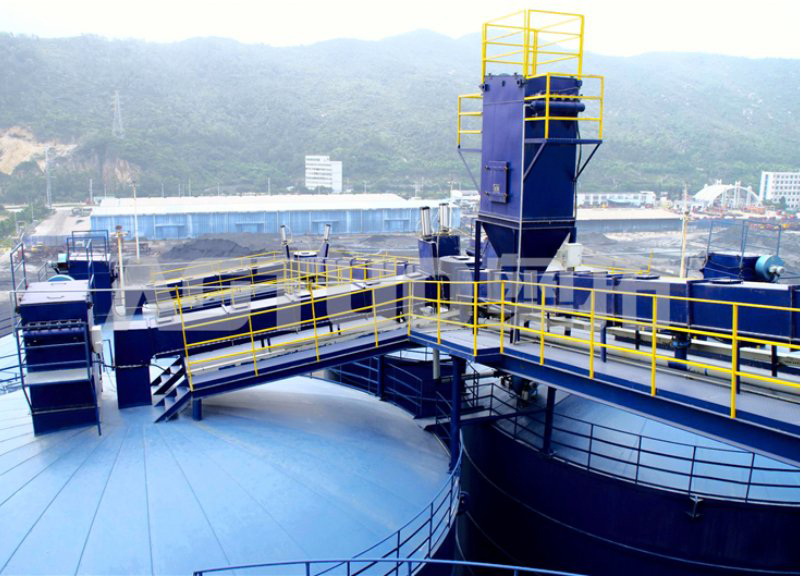
Additionally, comprehensive solutions such as Dust Extraction Systems and tailored Conveyor Solutions can cater to specific industry needs, offering dust management features that enhance workplace safety. The combination of high-quality equipment, like the Dust Deputy Bucket, with top-performing conveying solutions fosters an integrated approach that keeps production flowing smoothly while maintaining the highest standards of air quality. Whether you are looking to upgrade your current systems or establish a new setup, understanding these components will lead to informed decisions that enhance your operational capabilities.
How To Select Conveying Systems Construction Exceeds Industry Benchmarks Factory-Direct Excellence
| Year | Market Size (Billion $) | Growth Rate (%) | Key Trends |
|---|---|---|---|
| 2023 | 25.0 | 5.2 | Automation, Sustainability |
| 2024 | 26.5 | 6.0 | Smart Technologies |
| 2025 | 28.0 | 6.8 | IoT Integration |
| 2026 | 30.5 | 7.5 | Eco-friendly Designs |
| 2027 | 32.0 | 8.2 | AI Applications |
Don't Miss These Conveying Systems Construction Your End-to-End Solution Outperforms the Competition
E
Emily Johnson
I am very satisfied with my purchase. The product quality is fantastic, and the after-sales service team was knowledgeable and courteous.
03
April
2026
H
Henry Evans
I love this product! The quality is impressive and the after-sales service team was very supportive and knowledgeable.
06
May
2026
H
Hannah Cook
I am very satisfied with my purchase. The quality and the after-sales assistance were truly exceptional.
29
May
2026
R
Riley Diaz
I am thrilled with the quality of this item! The customer service team was highly capable and ensured all my needs were met.
16
April
2026
E
Ethan Lee
Amazing quality and functionality! Their team provided comprehensive assistance, which added value to my purchase.
31
May
2026
S
Sarah Davis
Absolutely delighted with the quality! It’s refreshing to see such commitment to customer satisfaction. The after-sales team was truly helpful and responsive.
05
April
2026