Best High-Quality Pallet Track Floor Conveyor Manufacturer, Factory
As a leading manufacturer and factory of high-quality pallet track floor conveyors, Hangzhou Aotuo Mechanical and Electrical Co., Ltd. is dedicated to providing innovative solutions for industrial material handling. Our cutting-edge technology focuses on enhancing operational efficiency while ensuring superior performance and reliability. We understand the diverse needs of global buyers and cater to various industries, offering tailored solutions that integrate seamlessly into existing workflows. With an emphasis on durability and engineering excellence, our Pallet Conveyor systems are designed to withstand the rigors of demanding environments, delivering consistent results, In addition to our robust pallet conveyor systems, we specialize in advanced Pallet Conveyor Belts and efficient Track Saw Dust Collection systems. Our commitment to quality extends across our entire product range, ensuring that every component meets stringent industry standards. By leveraging our expertise and state-of-the-art facilities, we are proud to serve customers around the world, helping them optimize their material handling processes. Partner with Hangzhou Aotuo Mechanical and Electrical Co., Ltd. for reliable solutions that meet your operational needs and drive your business forward

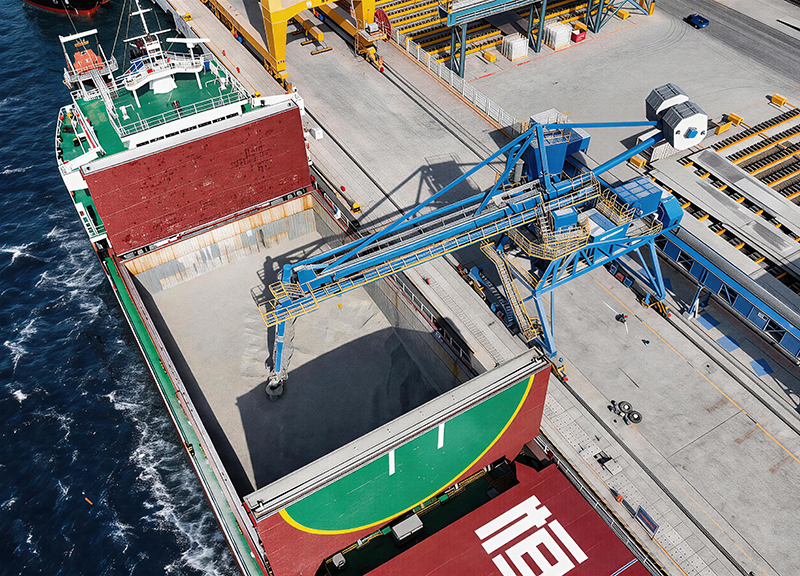
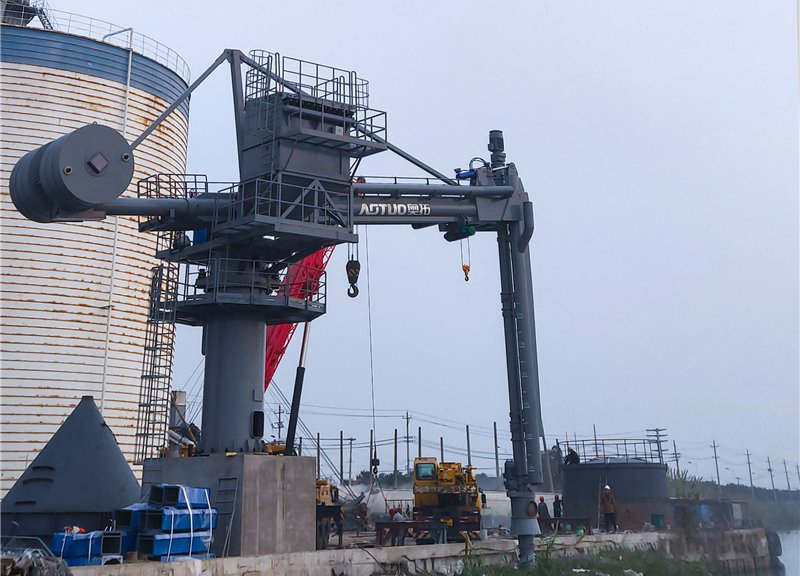
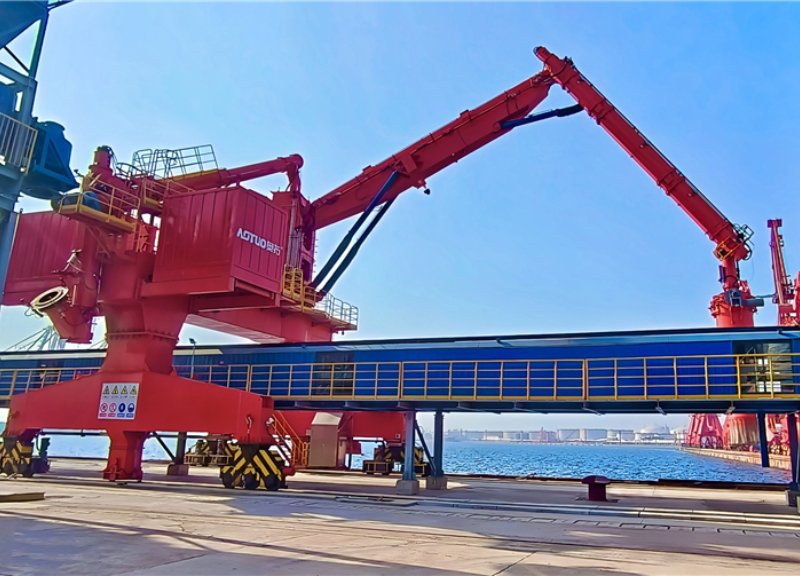
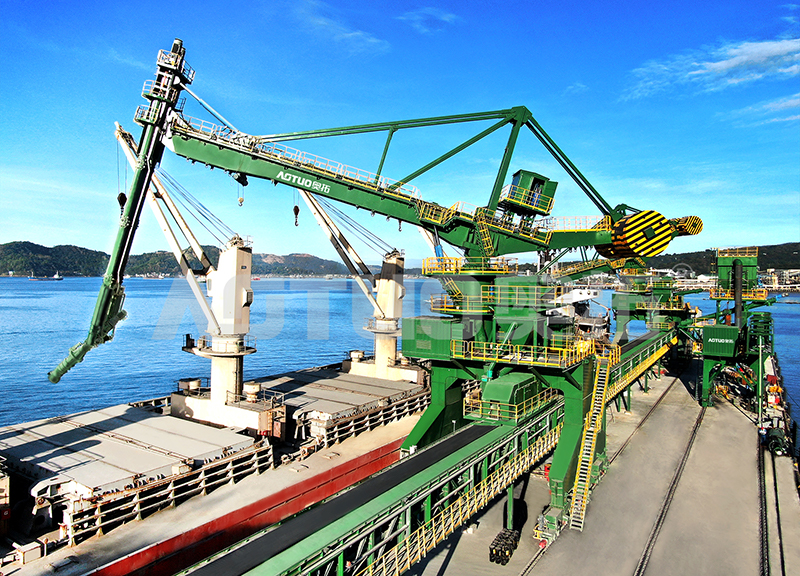
Don't Miss These Pallet Track Floor Conveyor From Concept to Delivery Supplies the World’s Top Brands
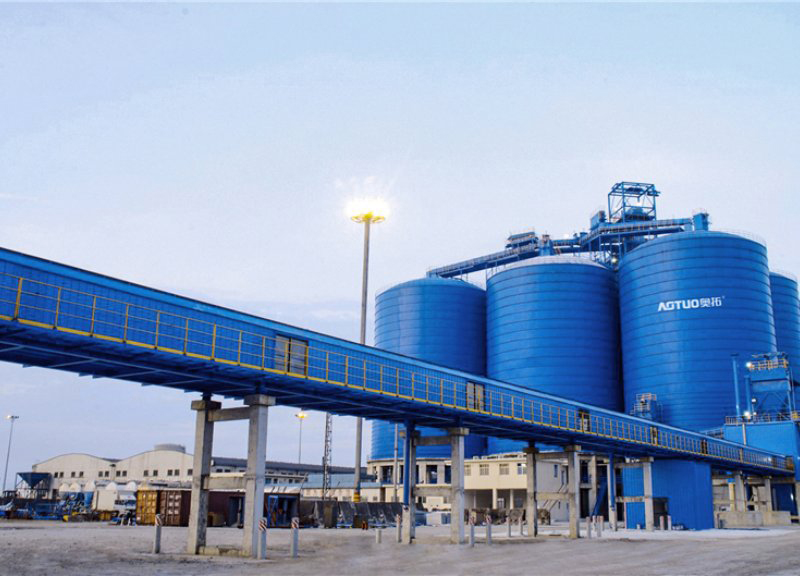
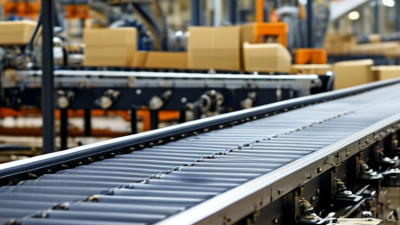
As global supply chains evolve, companies are increasingly turning to advanced conveyor systems to enhance their operational efficiency. Among these, the Pallet Track Floor Conveyor stands out for its ability to streamline heavy-duty material handling. This innovative solution is perfect for various applications, including automated assembly lines and warehouse logistics. With its robust design, the pallet transfer conveyor ensures smooth transportation and precise placement of products, facilitating a seamless workflow.
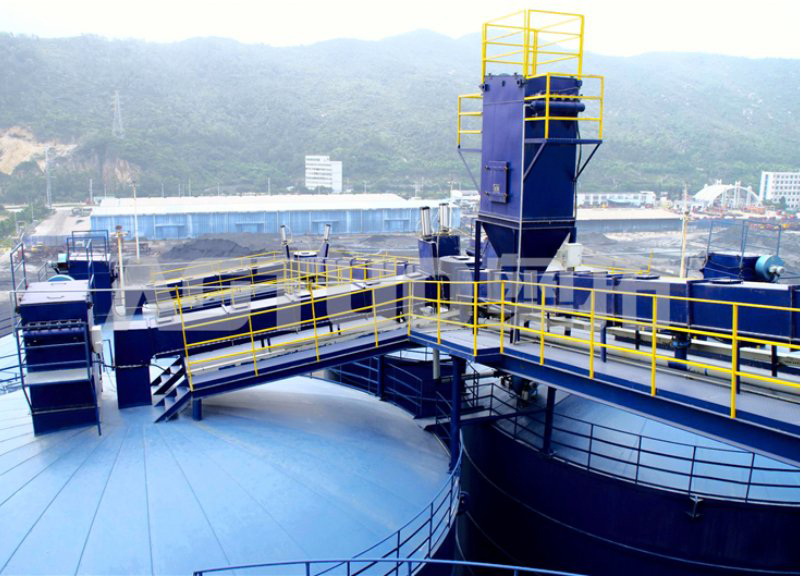
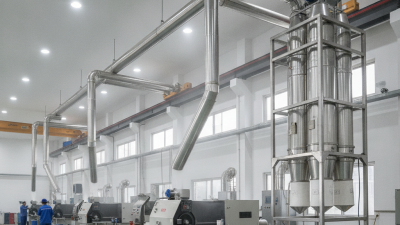
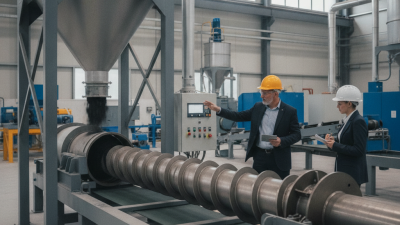
Furthermore, the integration of screw conveyor technology in bulk handling systems has revolutionized how businesses manage material transfer. From screw elevator conveyors that elevate materials to comprehensive ash conveyor systems designed for challenging environments, the versatility of these conveyor systems cannot be overlooked. As industries focus on optimizing productivity while maintaining safety standards, utilizing advanced dust collection solutions, such as dust collector bags and dry dust collectors, further enhances operational effectiveness by creating a cleaner workspace.
Investing in these conveyor solutions not only improves material handling efficiency but also boosts overall productivity by reducing downtime. Whether it's utilizing flexible belt conveyors to adapt to changing layouts or implementing air conveyor systems for lightweight materials, the right conveyor technology equips businesses to meet the demands of the modern market. Don't miss the opportunity to elevate your operations with state-of-the-art conveyor systems tailored to your specific needs.
Don't Miss These Pallet Track Floor Conveyor From Concept to Delivery Supplies the World’s Top Brands
| Trend / Metric | 2023 | 2024 Forecast | 2025 Projected Growth (%) |
|---|---|---|---|
| Market Size (Billion USD) | 2.8 | 3.1 | 10.7% |
| Adoption Rate (%) | 45 | 50 | 5.5% |
| Key Growth Drivers | Automation in Warehousing, Industry 4.0, Increased E-commerce Demand | ||
| Regional Growth Leaders | North America, Europe, Asia-Pacific | ||
| Sustainability Focus (%) | 30 | 40 | 33.3% |
Key Methods For Pallet Track Floor Conveyor Sets the Industry Standard in 2025
L
Leo Scott
Fantastic purchase! The product quality is superb, and the after-sales support team knew their stuff.
21
April
2026
S
Samuel Turner
Quality is top of the line! The after-sales personnel were not only professional but also understanding and kind.
15
April
2026
E
Ella Carter
Great durability and functionality! The after-sales service went above and beyond to make sure I was satisfied.
12
May
2026
O
Owen Woods
High quality product! The after-sales support was quick and very professional, answering all my questions.
17
April
2026
J
John Smith
I was truly impressed with the quality of the product. It exceeded my expectations, and the after-sales service was exceptional. The representative was knowledgeable and resolved my queries promptly.
04
May
2026
C
Christopher Lee
I was amazed by the quality and the thoughtfulness in the design of this item. The after-sales support was top-notch—very professional staff who really knew their stuff.
01
April
2026