China Best Automatic Sorting Conveyor Manufacturer, Factories
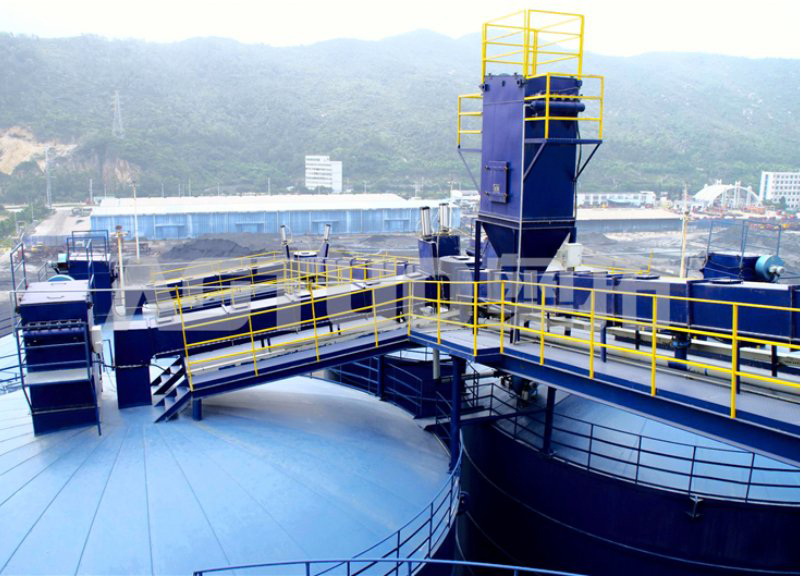
Hangzhou Aotuo Mechanical and Electrical Co., Ltd. stands proudly as a leading manufacturer of high-quality automatic sorting conveyor systems in China. With years of industry experience, we specialize in providing innovative solutions tailored to meet the diverse needs of global buyers. Our extensive product range includes Automatic Pallet Conveyors, Waste Sorting Conveyors, and Automatic Screw Conveyors, designed to enhance operational efficiency and streamline material handling processes in various industries. By leveraging advanced technology and employing rigorous quality control measures, we ensure that our products not only meet but exceed international standards, As a commitment to excellence, Hangzhou Aotuo prioritizes customer satisfaction by delivering reliable and durable conveyor systems that facilitate seamless automation. Our Waste Sorting Conveyors are engineered to optimize the sorting process for recycling and waste management, while our Automatic Screw Conveyors offer versatile material transport solutions ideal for different applications. Our experienced team is dedicated to providing exceptional support and service, helping clients navigate the complexities of automated systems. For businesses seeking dependable and high-performance conveyor solutions, Hangzhou Aotuo Mechanical and Electrical Co., Ltd. is your trusted partner in achieving operational success

Methods To choose Automatic Sorting Conveyor Application Manufacturer
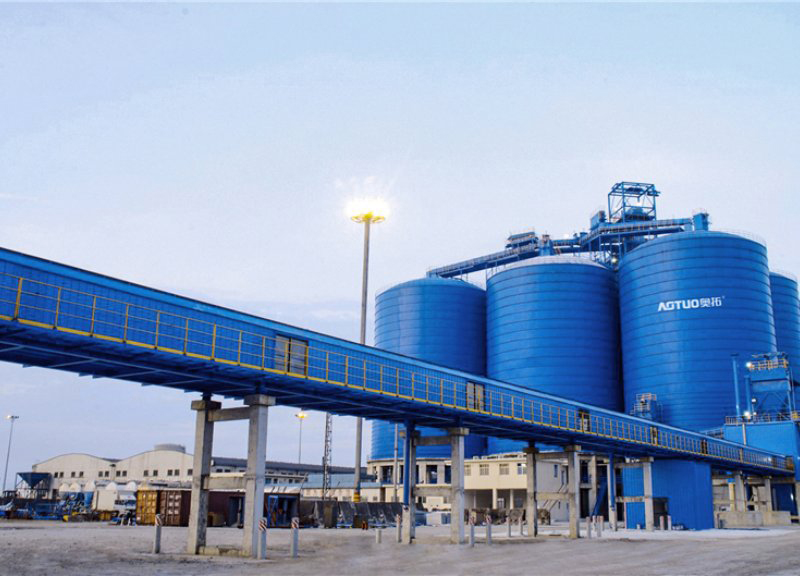
Selecting the right automatic sorting conveyor application manufacturer is crucial for enhancing your operational efficiency. With a variety of manufacturers in the market, it's essential to assess their expertise in producing conveyor systems that cater to specific needs. Look for a manufacturer that offers a broad range of products, including Screw Elevator Conveyor, Ash Conveyor Systems, and various Conveyor Systems that can handle dry bulk materials effectively. Their experience in research and development is vital, as it ensures that the equipment you acquire is not only reliable but also innovative.
Ensure that the manufacturer understands the importance of efficient dust management in conveyor applications. A reputable supplier should provide solutions that include integrated Dust Collector systems, capable of maintaining air quality while achieving high dust collection efficiency, utilizing products like a Dust Collector Cfm, Dry Dust Collector, and Dust Deputy Bucket. Evaluating their capability in designing systems that incorporate Dust Collector Bag and proper filtration solutions can significantly affect your operational outcomes.
Finally, consider the manufacturer's commitment to customer service and support. A reliable partner will not only offer quality products such as Flexible Conveyor and Dust Collection System but will also provide after-sales support, tuning, and maintenance services to keep your operations running smoothly. Investing in an automatic conveyor system from a well-regarded manufacturer can lead to improved productivity and reduced operational costs, solidifying your success in the competitive marketplace.
Methods To Choose Automatic Sorting Conveyor Application Manufacturer
| Aspect | Trend Data | Market Forecast |
|---|---|---|
| Growth Rate of Automated Systems | 15% CAGR (2023-2028) | Expected to reach $5 billion by 2028 |
| Adoption in E-commerce | 80% of top e-commerce players using automated sorting | Continued increase in integration through 2025 |
| Technological Advancements | Rise in AI and machine learning applications | Estimated to enhance efficiency by 30% |
| Labor Costs Impact | Labor costs rising by 5% annually | Increasing push for automation |
| Sustainability Focus | Growing demand for eco-friendly solutions | Sustainability market projected to grow by 20% |
Leading Chinese Automatic Sorting Conveyor Application Stands Out
E
Emily Johnson
I am very satisfied with my purchase. The product quality is fantastic, and the after-sales service team was knowledgeable and courteous.
03
April
2026
H
Henry Evans
I love this product! The quality is impressive and the after-sales service team was very supportive and knowledgeable.
06
May
2026
Z
Zachary Hayes
This product is truly remarkable in quality. The after-sales team showed a high level of professionalism which is greatly appreciated.
14
May
2026
A
Alexander Wong
Remarkable product quality! The after-sales support team responded promptly and professionally to all my queries.
30
April
2026
G
Grace Martinez
Fantastic quality! The customer service representatives were friendly, professional, and very reliable.
01
May
2026
C
Christopher Lee
I was amazed by the quality and the thoughtfulness in the design of this item. The after-sales support was top-notch—very professional staff who really knew their stuff.
01
April
2026