China High-Quality Recycling Conveyor Systems Factory, Manufacturer
Hangzhou Aotuo Mechanical and Electrical Co., Ltd. is a leading manufacturer specializing in high-quality recycling conveyor systems in China, committed to providing innovative solutions for industries worldwide. With a robust focus on durability and efficiency, our conveyor systems are designed to optimize material handling processes, enhance productivity, and reduce operational costs. Our product range includes advanced Lift Conveyor Systems that facilitate the vertical movement of materials, Rail Conveyor Systems perfect for horizontal transportation, and Mhe Conveyor Systems that combine versatility with strength to meet various industrial needs. By leveraging cutting-edge technology and adhering to international quality standards, we ensure that our systems deliver unparalleled performance in the recycling sector, As a trusted partner in the global marketplace, we take pride in offering customizable conveyor solutions that cater to the specific requirements of our clients. Our dedicated team of experts works closely with customers to understand their unique challenges, providing tailored designs that maximize operational efficiency. At Hangzhou Aotuo Mechanical and Electrical Co., Ltd., we are passionate about sustainability and continuously strive to revolutionize the recycling industry. From improving waste management processes to enhancing resource recovery, our innovative conveyor systems play a crucial role in promoting eco-friendly practices across various sectors. Partner with us today to explore how our Lift Conveyor Systems, Rail Conveyor Systems, and Mhe Conveyor Systems can transform your operations and contribute to a greener future

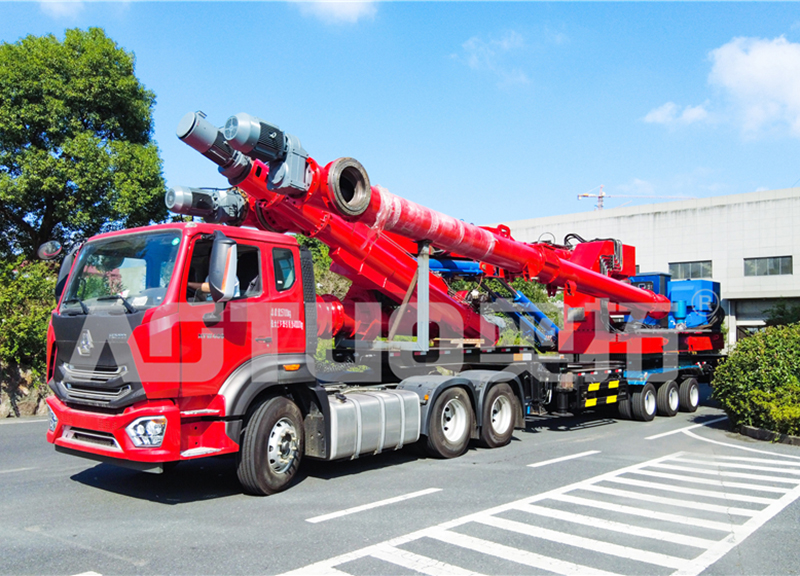
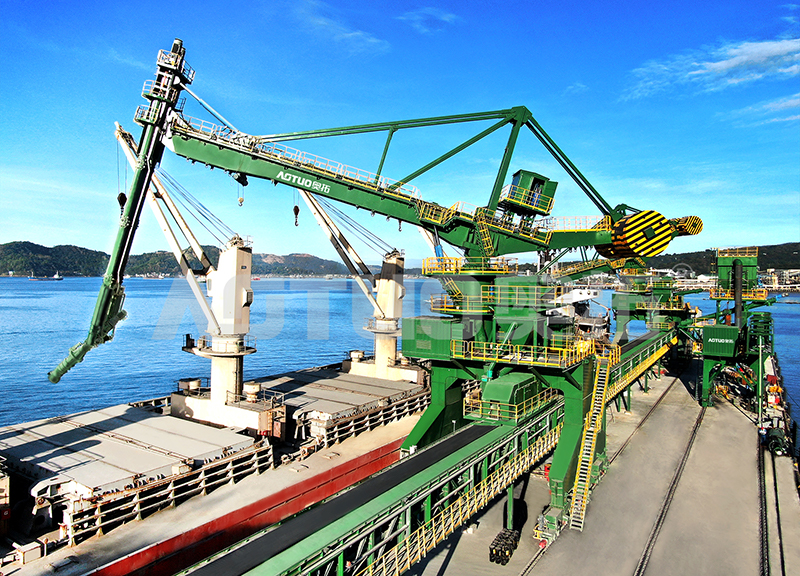
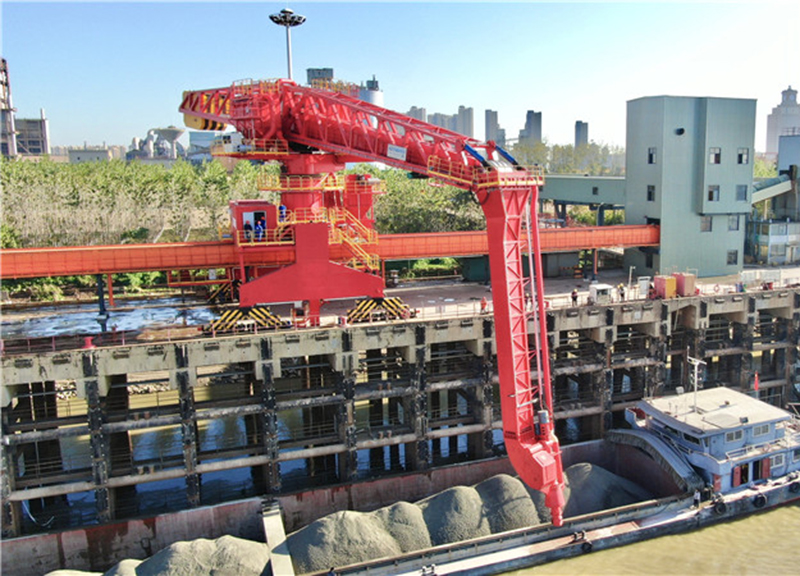
China Top Recycling Conveyor Systems Factory-Direct Excellence Custom Solutions,
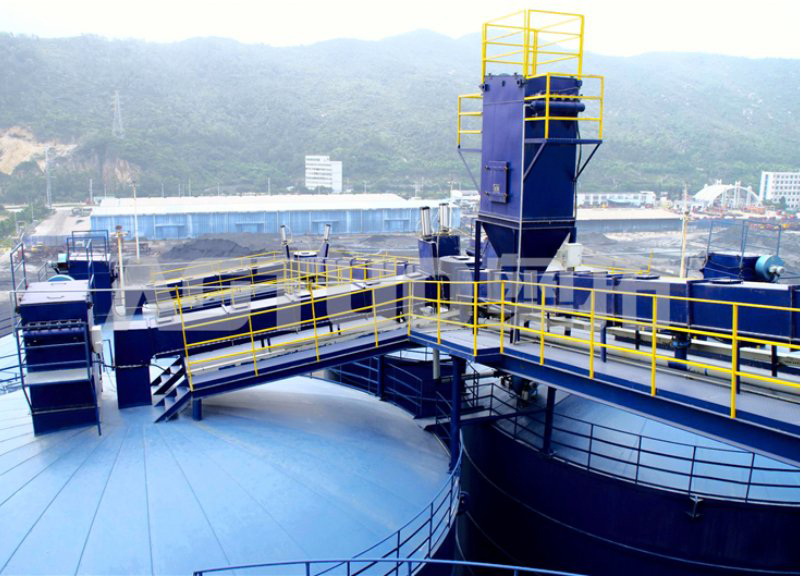
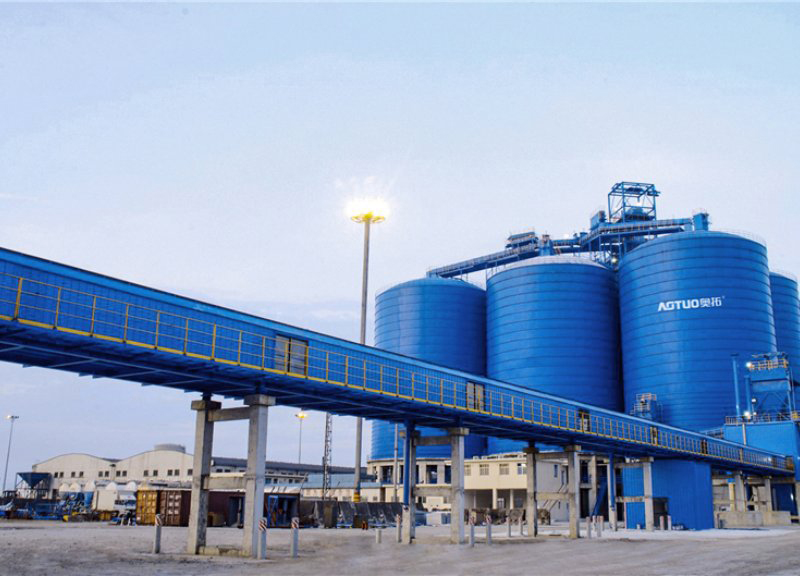
In the evolving landscape of industrial logistics, efficient handling mechanisms are crucial for optimizing workflows. Our innovative Conveyor Systems cater to diverse needs, offering tailored solutions that fit any operational requirement. From the robust Screw Elevator Conveyor designed for vertical lifting of bulk materials to specialized Ash Conveyor Systems handling the byproducts of combustion, our range of products is engineered for durability and performance.
Emphasizing the link between technology and efficiency, our Conveyor Systems enhance productivity and facilitate seamless operations. Whether you need Air Conveyor Systems for moving lightweight materials or Lift Conveyor Systems for elevating heavy loads, our expertise ensures you obtain reliable and efficient solutions. The integration of Dust Collector systems in these setups also highlights our commitment to maintaining a clean and safe working environment. The incorporation of elements such as the Dust Collector Bag, along with high-performance dust extraction systems, guarantees a reduction in airborne particles, safeguarding worker health and ensuring compliance with industry standards.
Furthermore, our advanced material handling solutions, including the Flexible Conveyor and various types of Roller Conveyor systems, optimize space and offer flexibility in configuration. The use of quality Conveyor Roller Materials increases the lifespan and reliability of our products, making them a worthy investment for global procurement professionals seeking high-performance machinery. With a focus on continuous improvement and sustainability, we are dedicated to providing solutions that push the boundaries of efficiency in the industry.
China Top Recycling Conveyor Systems Factory-Direct Excellence Custom Solutions
| Trend/Forecast | 2022 | 2023 | 2024 (Predicted) | 2025 (Predicted) |
|---|---|---|---|---|
| Global Recycling Market Size (Billion USD) | 200 | 210 | 225 | 240 |
| China Recycling Equipment Demand Growth (%) | 5 | 6 | 7 | 8 |
| Market Share of Automated Systems (%) | 30 | 35 | 40 | 45 |
| Investment in Recycling Technologies (Million USD) | 1000 | 1200 | 1500 | 1800 |
| Employment in Recycling Sector (Million) | 1.5 | 1.6 | 1.8 | 2.0 |
Methods To Recycling Conveyor Systems Supplier Your End-to-End Solution
I
Isabella Wilson
This product is a testament to quality. The after-sales service was exceptional, with personnel who genuinely care about customer satisfaction.
01
May
2026
N
Nathan Hall
Impressive quality! The after-sales team was highly knowledgeable and provided fantastic support when I had questions.
27
April
2026
C
Claire Sanchez
Amazing quality! I greatly appreciated the professionalism of the support staff during my after-sales inquiries.
03
April
2026
E
Emma Johnson
The quality of the products exceeded my expectations. The after-sales service was also exceptional; their team was always ready to assist with any concerns.
13
April
2026
O
Olivia Roberts
Fantastic product quality! The team stood behind their merchandise with outstanding support when I needed guidance.
23
April
2026
J
Jack Walker
The attention to detail in the product is impressive! The after-sales support team was knowledgeable and responsive.
03
May
2026