High-Quality Best Belt Driven Conveyor Systems Factory, Manufacturer
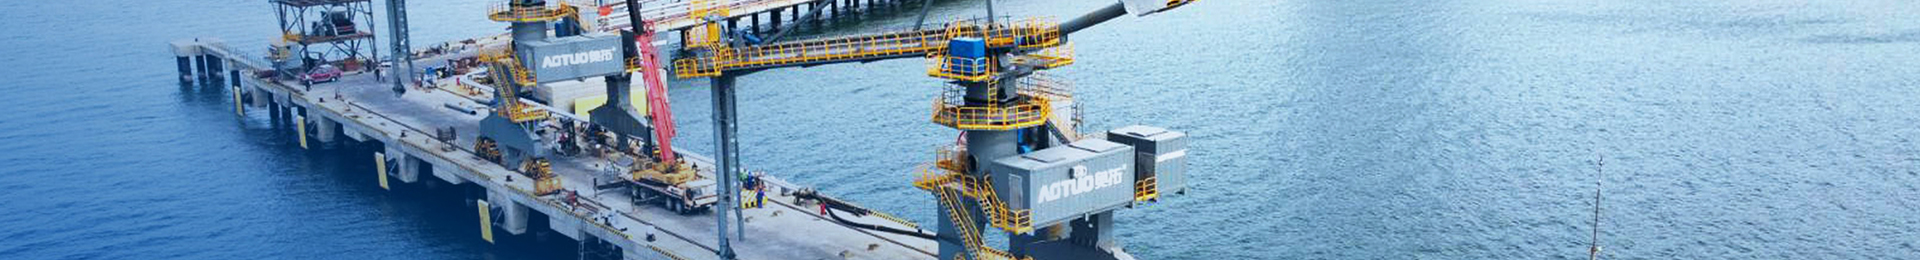
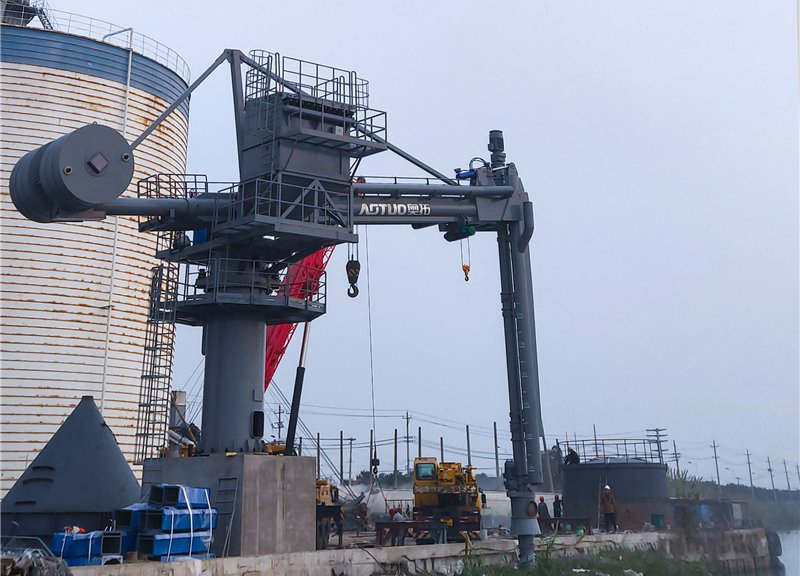
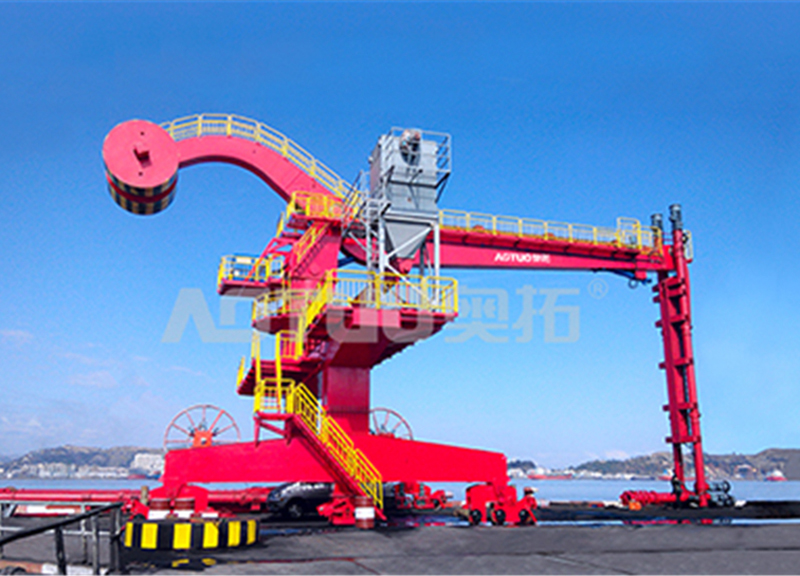
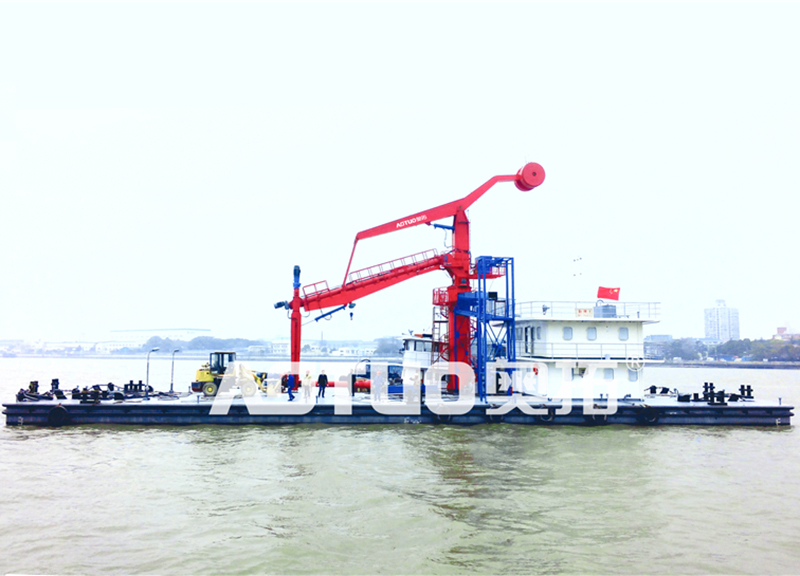
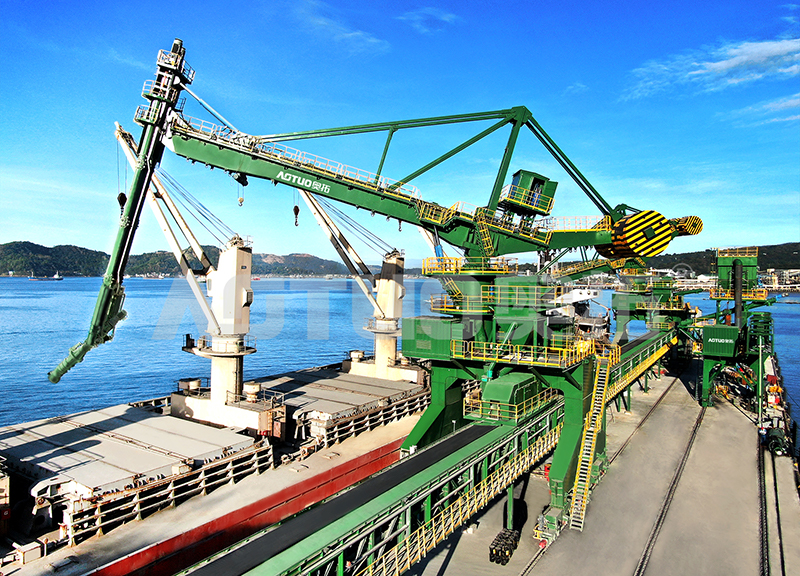
Welcome to Hangzhou Aotuo Mechanical and Electrical Co., Ltd., your premier source for high-quality belt-driven conveyor systems. With a strong commitment to innovation and excellence, our factory specializes in the design and manufacturing of efficient material handling equipment. As a leading manufacturer in the industry, we offer a wide range of solutions tailored to meet the diverse needs of global buyers. Our belt-driven conveyor systems are engineered for reliability and durability, ensuring that your operations run smoothly and effectively. From warehouses to manufacturing facilities, our products are designed to enhance productivity and streamline logistics, Our extensive portfolio includes advanced Driven Roller Conveyors, which are ideal for various applications, maximizing space efficiency while minimizing operational costs. Additionally, we provide state-of-the-art Mhe Conveyor Systems that integrate seamlessly into your production line, ensuring a steady flow of materials. For industries requiring robust solutions, our Chain Driven Conveyors offer exceptional strength and versatility, suited for handling heavy loads. At Hangzhou Aotuo, we pride ourselves not only on the quality of our products but also on our commitment to customer satisfaction. Partner with us to elevate your business efficiency and experience the reliability of our conveyor systems tailored to your specific needs

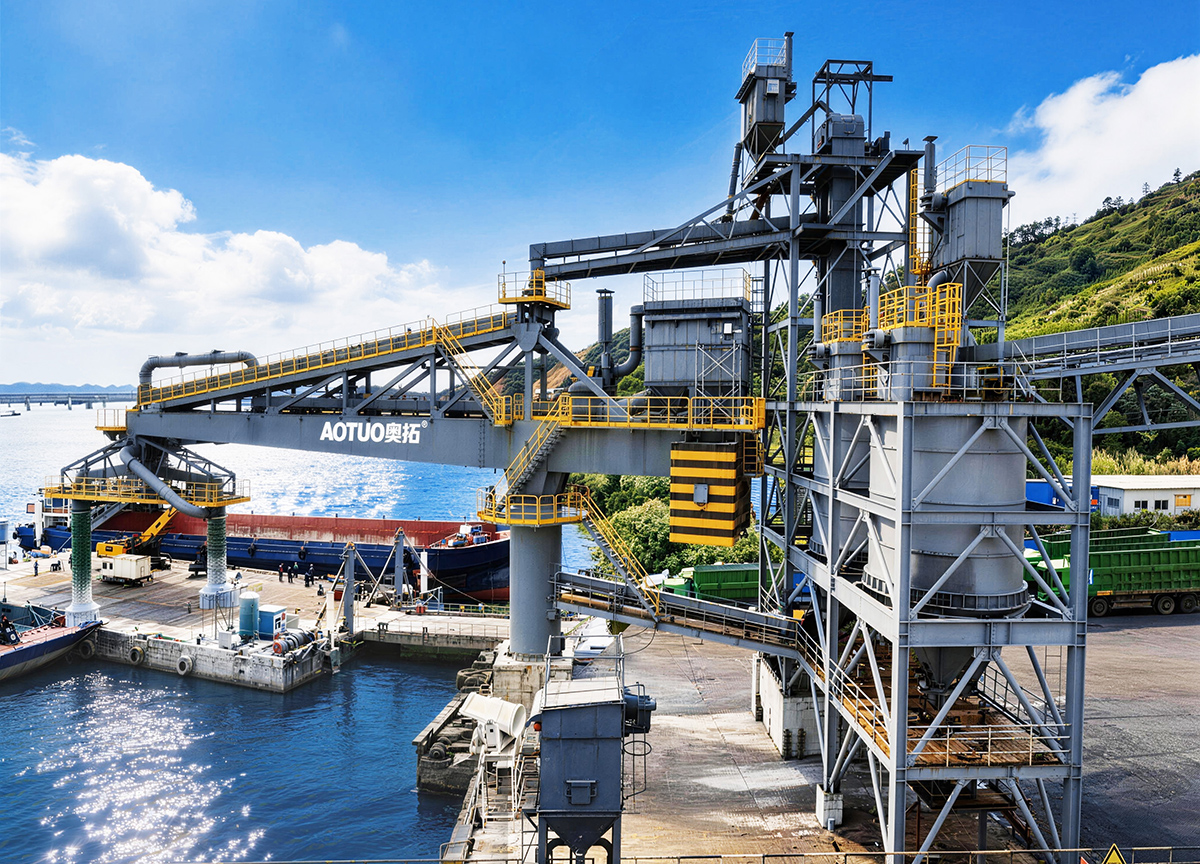
Expert Tips For Belt Driven Conveyor Systems Your Trusted OEM Partner Global Reach
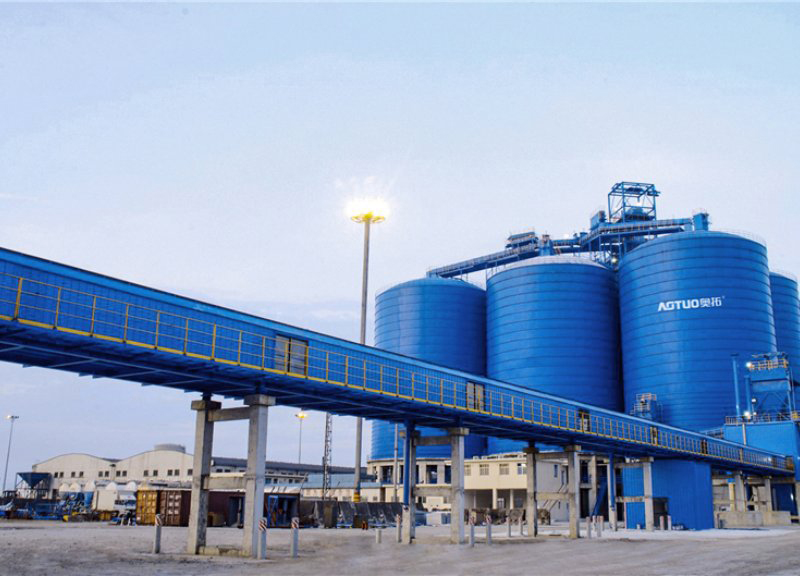
When it comes to optimizing your operations with belt-driven conveyor systems, adopting the right strategies is crucial. These systems excel in transporting dry bulk materials, making them indispensable in many industries. To ensure efficiency and reliability, focus on maintaining your equipment rigorously. Regularly inspect components such as the Conveyor Side Rollers and Conveyor Idler Rollers for wear and tear, as they play a vital role in smooth operation. In the context of high-demand environments, consider integrating advanced solutions like the Screw Elevator Conveyor for efficient vertical lifting of materials alongside applications utilizing Ash Conveyor Systems.
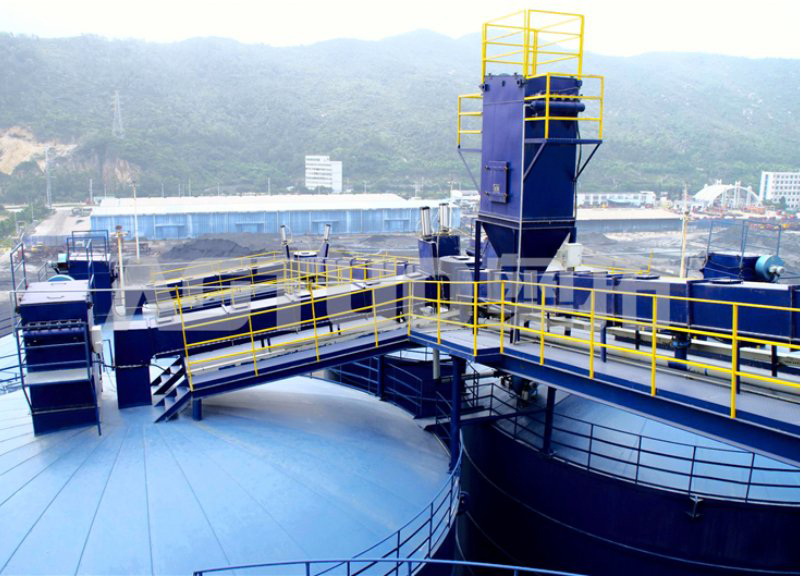
Moreover, the proper integration of various Conveyor Systems such as Air Conveyor Systems and Lift Conveyor Systems can increase your operational capacity while minimizing downtime. Incorporate effective dust management strategies by deploying Dust Collector systems like Dry Dust Collector or Filter Bag Dust Collector, particularly when handling fine particulate matter. This will not only uphold a cleaner working environment but also comply with safety regulations, ensuring a holistic approach to operational efficiency. Whether you are investing in Flexible Conveyor or specialized solutions like Screw Conveyor, understanding the compatibility and advantages of various conveyor types is essential for maximizing output and reliability.
Expert Tips For Belt Driven Conveyor Systems: Industry Trends and Market Forecasts
| Dimension | Trend/Forecast | Year |
|---|---|---|
| Global Conveyor System Market Growth | 8.1% CAGR | 2021-2026 |
| Adoption of Automation | Increased by 50% | 2023 |
| Material Handling Efficiency | Improvement of 30% | 2025 |
| Sustainability Initiatives | Growing adoption of eco-friendly materials | 2024 |
| Investment in Smart Technologies | Projected to reach $5 Billion | 2026 |
Quick Tips To Belt Driven Conveyor Systems Delivers Unmatched Quality Pioneers in the Field
B
Benjamin Anderson
Top-quality item that performs as expected! The after-sales support was exemplary, quickly addressing my queries in a professional manner.
19
May
2026
N
Nathan Hall
Impressive quality! The after-sales team was highly knowledgeable and provided fantastic support when I had questions.
27
April
2026
S
Scarlett Brown
Impressive quality that stands out! The customer service was professional and went out of their way to ensure satisfaction.
23
May
2026
A
Asher Ortiz
Impressive quality and fantastic service! The customer care team was prompt in their responses and highly professional.
02
April
2026
G
Grace Martinez
Fantastic quality! The customer service representatives were friendly, professional, and very reliable.
01
May
2026
M
Mark James
Impressive quality and functionality! The team was knowledgeable and ensured I was well taken care of after my purchase.
27
May
2026