High-Quality China Bottle Accumulation Conveyor Product, Manufacturer
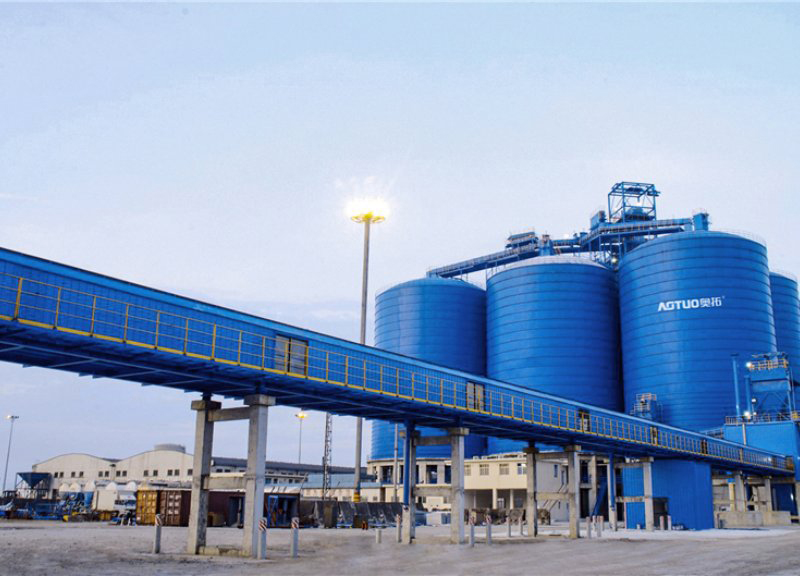
At Hangzhou Aotuo Mechanical and Electrical Co., Ltd., we specialize in producing high-quality bottle accumulation conveyors designed to enhance the efficiency of your production line. Our state-of-the-art manufacturing facilities in China enable us to offer a diverse range of conveyors, including the innovative Ash Conveyor and the reliable Drag Conveyor. These products are engineered to meet the rigorous demands of the beverage and packaging industries, ensuring seamless transportation and accumulation of bottles while maintaining the highest industry standards. With a focus on durability and performance, our conveyor solutions can be tailored to suit your unique operational requirements, As a leading manufacturer, Hangzhou Aotuo is committed to providing exceptional customer service and support throughout your purchasing journey. Our Bottle Filling Conveyor is designed to facilitate smooth operations and increase productivity, allowing you to optimize your workflow. We understand the importance of quality and reliability in conveyor systems, which is why we source premium materials and employ advanced technology in our production process. Partner with us to experience the latest in conveyor technology and elevate your production capabilities, as we serve global buyers seeking excellence in mechanical and electrical solutions

10 Essential Tips For Bottle Accumulation Conveyor Ahead of the Curve in 2025
In the rapidly evolving landscape of manufacturing and logistics, staying ahead of the curve requires innovative solutions and efficient systems. As we look toward 2025, optimizing Bottle Accumulation Conveyor systems will be key for global procurement managers seeking to enhance productivity and reduce operational costs. Implementing advanced Conveyor Systems, including Air Conveyor Systems and Lift Conveyor Systems, can significantly improve the flow and handling of goods, ensuring a smooth operation that meets the demands of modern production.
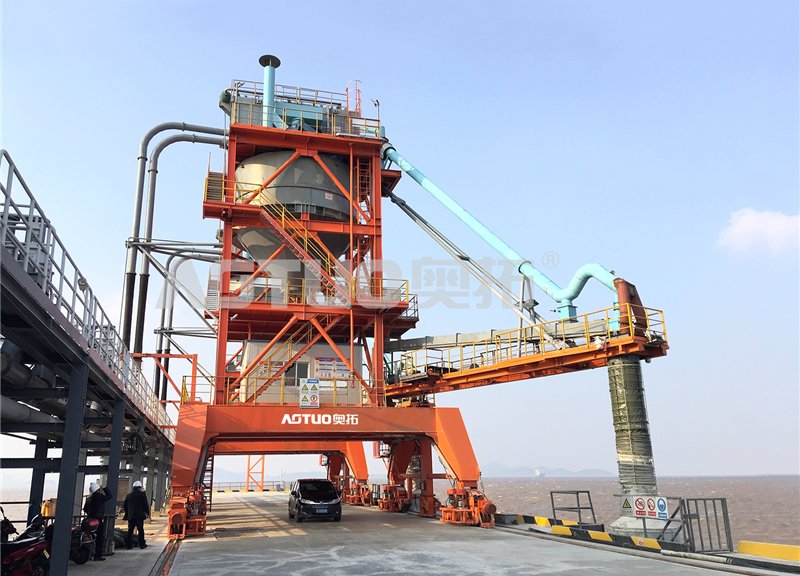
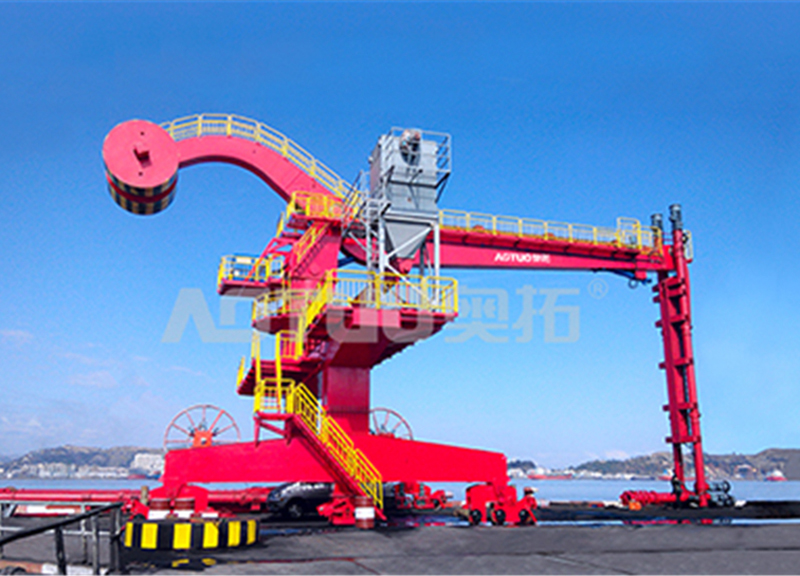
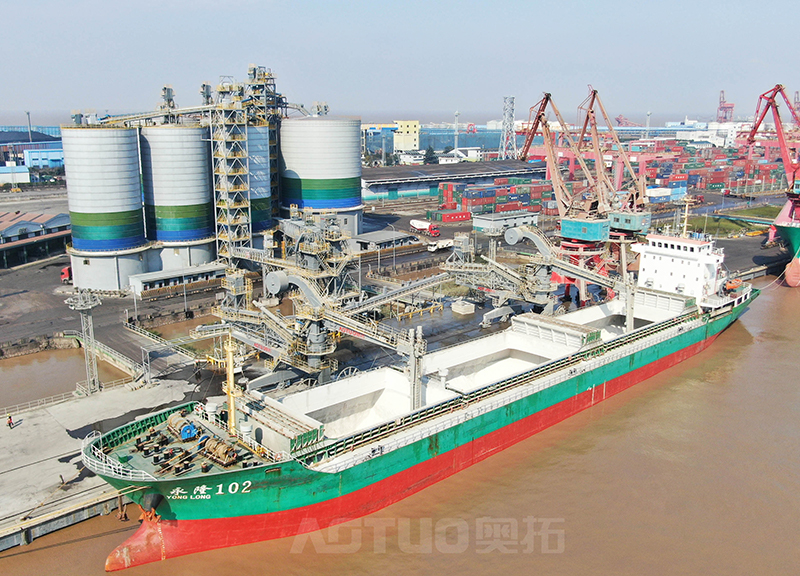
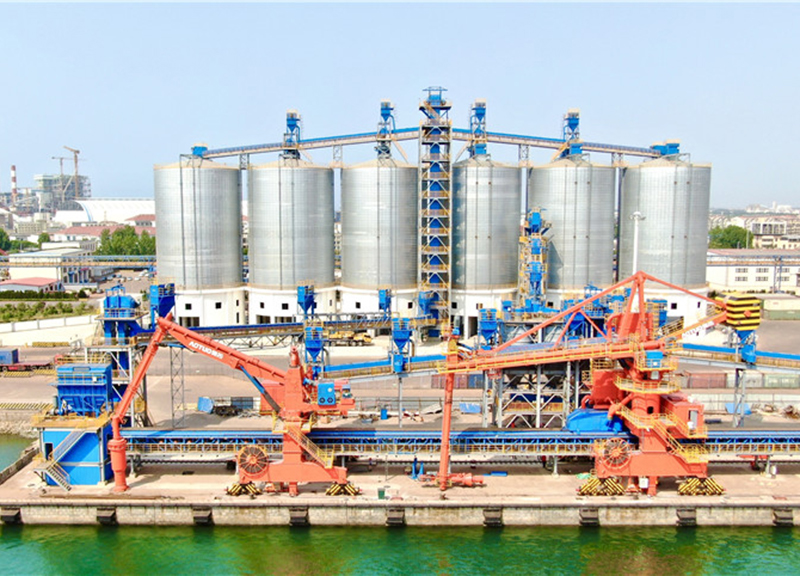
Key components like the Screw Elevator Conveyor and Ash Conveyor Systems play a vital role in efficient material transportation. These systems are designed to facilitate the handling of various bulk materials while minimizing downtime and maximizing operational efficiency. As industries continue to focus on sustainability, investing in robust and environmentally-friendly solutions like the Screw Conveyor ensures companies not only enhance their production capabilities but also reduce their carbon footprint.
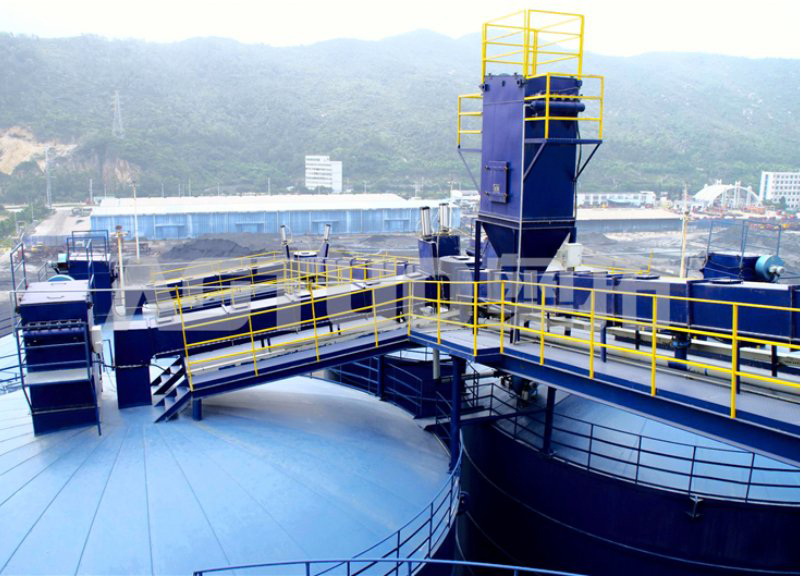
Furthermore, integrating effective dust control measures with products such as the Dust Collector Bag and Dry Dust Collector within production lines allows for a cleaner, safer working environment. Employing technologies like the Dust Deputy Bucket and Jet Dust Collector can drastically improve the dust extraction process, ultimately leading to healthier workspaces. As supply chain dynamics shift, utilizing high-quality, customizable manufacturing solutions will be essential in maintaining a competitive edge in 2025. Emphasizing flexibility and adaptability in your Conveyor Systems will not only streamline operations but also position your business for long-term success in a challenging global market.
10 Essential Tips For Bottle Accumulation Conveyor Ahead of the Curve in 2025
| Trend/Factor | Description | Market Impact | Forecast Year |
|---|---|---|---|
| Automation Integration | Increasing use of automation technologies in bottling processes. | Efficiency improvements, reduced labor costs. | 2025 |
| Sustainability Practices | Shift towards eco-friendly materials and practices in manufacturing. | Enhanced brand reputation, potential cost increases. | 2025 |
| Smart Technology Adoption | Implementation of IoT solutions for real-time monitoring and analytics. | Better decision-making based on data, predictive maintenance. | 2025 |
| Increased Demand for Customization | Growing consumer preference for personalized products. | Need for flexible manufacturing systems. | 2025 |
| Workforce Adaptability | Training programs for workforce to handle advanced technologies. | Improved operational efficiency and morale. | 2025 |
| Enhanced Safety Standards | Rigorous safety measures and regulations impacting operations. | Potential increases in operational costs for compliance. | 2025 |
| Digital Transformation | Adoption of digital tools for supply chain management. | Greater transparency, improved resource management. | 2025 |
| Artificial Intelligence Utilization | Use of AI for predictive maintenance and operational efficiency. | Cost reduction and enhanced uptime. | 2025 |
| Global Supply Chain Challenges | Navigating disruptions and adapting to global trade dynamics. | Increased focus on supply chain resilience. | 2025 |
| Consumer Health Awareness | Rising demand for health-oriented and safe products. | Shift in product offerings and packaging designs. | 2025 |
Why Trust Bottle Accumulation Conveyor Stands Out Dominates
S
Sophia Turner
Exceptional quality and a seamless purchasing experience. The support team went above and beyond to answer my questions and guide me through the process.
25
April
2026
H
Henry Evans
I love this product! The quality is impressive and the after-sales service team was very supportive and knowledgeable.
06
May
2026
C
Claire Sanchez
Amazing quality! I greatly appreciated the professionalism of the support staff during my after-sales inquiries.
03
April
2026
E
Ella Carter
Great durability and functionality! The after-sales service went above and beyond to make sure I was satisfied.
12
May
2026
J
Jack Walker
The attention to detail in the product is impressive! The after-sales support team was knowledgeable and responsive.
03
May
2026
S
Sarah Davis
Absolutely delighted with the quality! It’s refreshing to see such commitment to customer satisfaction. The after-sales team was truly helpful and responsive.
05
April
2026